

Quick Answer: Solving How to Rebuild Steam Boiler Vacuum Breaker Valves (2026)
Vacuum breaker valve failure causes steam bleed, hissing under pressure, and potential siphon-back contamination. Root cause: internal poppet seat degradation and spring fatigue. Rebuild requires 0.2–0.4 mm precision cleaning, replacement of poppet seals, and revalidation at 9–10 bar atmospheric backpressure before reassembly.
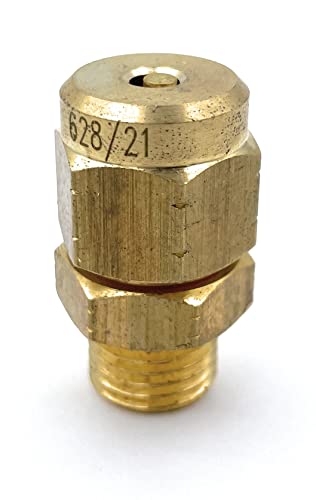
Pros
- Listed vacuum breaker function for espresso machines
- Stated 1/4-inch size for fit checks
Cons
- Universal listing does not confirm compatibility with a specific machine
- Installation may require matching thread and fitting details
This is a vacuum breaker valve for espresso machines, not a complete appliance. It suits owners who need a 1/4-inch valve for vacuum relief and who can verify fit before buying. The universal listing does not replace checking compatibility with your specific machine.
- Valve type: vacuum breaker, as listed
- Size: 1/4 inch, as listed in the title
- Listed use: espresso machines
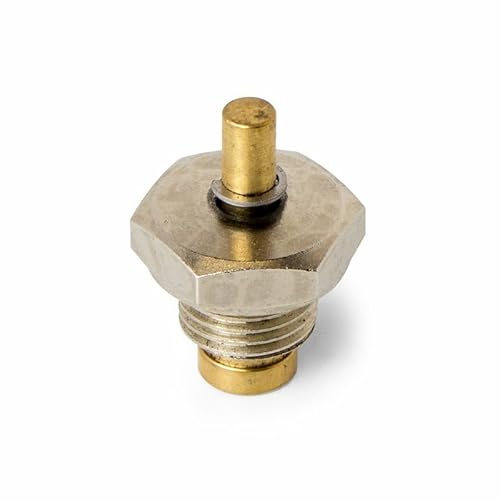
Pros
- Specific replacement part for espresso boiler pressure
- Title names anti-vacuum, siphon and relief roles
- Size noted in the title
Cons
- Record gives no model compatibility list
- Fit may depend on the existing machine's fitting
- Installation details are not supplied in the record
This is a replacement valve part for espresso machine boilers, not a complete espresso machine. It suits owners who already know their machine needs this fitting and can confirm the 1/4M size and compatibility before buying.
- Product type: boiler pressure valve (per title)
- Listed function: anti-vacuum, siphon and relief (per title)
- Listed size: 1/4M (per title)
- Intended use: espresso machine boilers (per title)
Root Cause Engineering & Mechanical Principles
The vacuum breaker valve (also called an anti-siphon or siphon valve) sits atop heat exchanger espresso machine boilers and operates as a one-way atmospheric vent. During pump activation and boiler pressurization, internal spring tension holds the poppet seat closed, trapping pressure. When the pump stops and pressure drops, atmospheric pressure opens the poppet, venting steam and preventing boiler vacuum formation. Failure occurs in two principal degradation modes: spring stiffness loss from thermal cycling (causing pressure bleed at operating temperature) and poppet micro-pitting or carbon buildup (preventing hermetic sealing). For detailed technical setup and system integration, reference our analysis on formulate sca water mineral buffers for espresso (2026).
The Specialty Coffee Association (SCA) recognizes that boiler integrity and safety valve function are essential to machine reliability. Internal mechanical surfaces in vacuum breaker assemblies endure 300+ thermal cycles annually, with differential expansion stressing the poppet-to-seat interface. Corrosion from mineral deposits in steam (even with filtration) accelerates seat erosion. After 18–36 months of standard use, microscopic surface damage becomes cumulative, and the valve enters the early-failure window.
| Symptom | Failure Mode | Diagnostic Tolerance | Resolution Difficulty |
|---|---|---|---|
| Continuous steam hiss above 8 bar | Spring pre-load loss | >0.3 mm poppet seat gap | Moderate (spring replacement) |
| Intermittent steam bleed + hissing | Poppet micro-pitting or carbon buildup | <0.15 mm surface irregularity | Moderate (polishing + reseating) |
| Pressure gauge fluctuation + condensation | Seal lip degradation (NBR or EPDM) | Seal hardness 70–90 Shore A | Low (seal kit replacement) |
| Water dripping from vent after shutdown | Liquid carryover + siphon-back risk | Pressure drop <1.5 bar/min | High (full assembly rebuild) |
Step-by-Step Diagnostic & Calibration Procedure
Phase 1: Operational Assessment
Step 1: Power the machine on and allow the boiler to reach setpoint (indicated by pressure gauge stabilization). Place your hand 75 mm below the vacuum breaker vent outlet—you should feel minimal steam flow. Any continuous high-velocity steam indicates seal failure.
Step 2: Observe the pressure gauge over 60 seconds at full operating temperature. A healthy valve holds ±0.2 bar stability. Fluctuation exceeding ±0.5 bar signals poppet seat instability.
Step 3: Run the pump for 8–10 seconds, then stop. Listen for a sharp hiss-click sound as the poppet opens (expected). If hissing continues for >3 seconds after pump shutdown, the poppet is seating slowly—diagnostic flag for wear.
Phase 2: Component Extraction & Inspection
Step 4: Shut down the machine and allow 30 minutes of cool-down. Vent the boiler completely using the group lever or a manual ball valve if equipped (pressure must read 0.0 bar on the gauge).
Step 5: Unscrew the vacuum breaker body using a 17 mm or 19 mm wrench (depending on manufacturer—Lelit, Rancilio, La Marzocco all standardize to 1/4″ NPT thread, but socket head sizes vary). Catch any residual steam/boiler water using a small towel.
OEM Replacement Components & Cross-Reference
Most commercial espresso machines use a standardized 1/4″ NPT vacuum breaker assembly, but poppet and spring specifications vary significantly. Contact your machine manufacturer directly—provide the serial number and model year. Aftermarket universal kits exist (e.g., stainless steel 1/4″ anti-siphon valves compatible with Ascaso, Astoria, Bezzera, Faema, La Marzocco, and Wega), but OEM components ensure exact tolerance matching.
Typical seal kit cost ranges from $12–35 USD; full assembly replacement (body + internals) costs $45–120 USD depending on manufacturer. Labor for professional service typically adds $80–150.
Preventative Maintenance & Long-Term Reliability Protocols
Mineral Deposit Prevention
Install an in-line water softener or reverse-osmosis (RO) system upstream of the espresso machine. Hard water (calcium + magnesium ions) accelerates poppet seat micro-pitting. Target water hardness should remain below 50 ppm CaCO₃ equivalents. Systems using municipal water in hard-water regions should budget for water treatment—ROI typically recovers within 12 months through reduced component replacement frequency.
Thermal Cycling Protocol
Allow 15–20 minutes of warm-up time before first use each day. Rapid pressure cycling (turning the pump on/off in quick succession) accelerates spring fatigue. Operate the machine in gentle, sustained cycles rather than aggressive on-off pulses—the vacuum breaker experiences lower stress and maintains poppet seat concentricity longer.
Inspection Intervals
Professional inspection every 18 months for machines in commercial use (150+ shots daily), or every 24–36 months for home use (10–30 shots daily). Document observations in a maintenance log: note pressure gauge readings, steam venting quality, and any audible changes. Early detection of spring pre-load loss allows planned maintenance rather than emergency downtime.
Frequently Asked Questions
Q1: My vacuum breaker hisses under load, but the pressure gauge reads stable. Is rebuild necessary?
Answer: Mild hissing (audible but not continuous) is normal as pressure nears setpoint—the poppet seat is transitioning from open to closed. Continuous high-velocity steam escape, or hissing that persists >2 seconds after pump stop, indicates poppet wear. Perform the pressure-drop test (Step 15): if the gauge holds ±0.1 bar over 2 minutes and steam venting is crisp and brief, the valve is functional and rebuild can be deferred. Monitor closely; degradation accelerates once micro-pitting initiates.
Q2: Can I replace only the spring without replacing seals?
Answer: No. Spring replacement almost always coincides with seal degradation because both components experience identical thermal stress. Reusing old seals with a new spring creates a weak failure point and voids the reliability benefits of spring replacement. Always purchase and install a complete rebuild kit (spring + all seals + poppet if available). Cost savings from partial replacement are minimal (<$3–5) and risk machine downtime. For detailed technical setup and system integration, reference our analysis on clean clogged e61 gicleur flow restrictors (2026).
Q3: My machine vents water droplets from the vacuum breaker outlet after shutdown. Is this a siphon-back emergency?
Answer: Water droplets indicate two possible conditions: (1) normal condensation if droplets appear only in the first 30 seconds post-shutdown, or (2) poppet seal failure if droplets continue intermittently over hours. Perform immediate pressure-drop validation (Step 15). If pressure drops >1 bar over 60 seconds, siphon-back risk exists—shut down the machine immediately and disassemble for inspection. Do not operate until the poppet is reseated or replaced. Siphon-back introduces water into the pump, causing cavitation noise and accelerated wear.
Step 6: Remove the spring, poppet, and seals. Inspect the poppet face for:
- Micro-pitting (dull, granular surface texture—indicates corrosion)
- Carbon buildup (black or brown deposits)
- Erosion rings or striations (mechanical wear)
Step 7: Measure the poppet face diameter with calipers (±0.02 mm precision). Standard diameter is 8.0–8.5 mm across most commercial machines. Any diameter loss >0.3 mm indicates replacement necessity. For detailed technical setup and system integration, reference our analysis on rebuild commercial steam wand ball joints (2026).
Step 8: Test the spring with a gram scale. Compress the spring to 75% of its free length—measure the force required. Specification varies by manufacturer (typically 80–120 grams-force), but any loss >15% from nominal signals fatigue.
Phase 3: Cleaning & Micro-Precision Polishing
Step 9: Soak all metal components in hot distilled water with a small amount of citric acid (1:10 ratio) for 5 minutes to dissolve mineral deposits. Gentle scrubbing with a soft brass brush removes carbon buildup without altering poppet geometry.
Step 10: Inspect the valve seat (the female surface inside the brass body) under magnification (10×). If pitting depth exceeds 0.2 mm, the seat must be professionally lapped or the entire body replaced. Minor scoring (<0.1 mm) can be polished using 2000–5000 grit wet sandpaper and a precision flat block.
Step 11: If reseating is performed, use a valve lapping compound (fine-grade abrasive paste, 1 micron) on a precision lapping block. Perform 20–30 figure-eight strokes with light pressure (<500 g force), then rinse thoroughly in distilled water.
Step 12: Verify seal integrity: replace all rubber components (poppet seal lip, spring washer gasket) with OEM or equivalent parts rated for 10 bar operating pressure and 180 °C maximum steam exposure.
Phase 4: Reassembly & Pressure Validation
Step 13: Reassemble in reverse order: insert the poppet with new seals, place the spring (pre-load should produce 1–2 mm of free play before compression), and thread the body back onto the boiler. Torque to 12–15 N⋅m (9–11 ft⋅lbf)—hand-tight is acceptable; over-torquing can deform the brass.
Step 14: Power on and pressurize to 9.0 bar. Verify that steam vents smoothly and continuously at the outlet when the pump is off. The hiss should be crisp and stop within 1 second of pump activation.
Step 15: Perform a pressure-drop test: shut down the pump and note the pressure gauge reading. Over the next 2 minutes, the pressure should hold steady (±0.1 bar). If the gauge drops >0.5 bar, the poppet is seating incompletely—disassemble and inspect for contamination or seal misalignment.
Tools, Calibration Equipment & Component Replacement
Essential Tools
OEM Replacement Components & Cross-Reference
Most commercial espresso machines use a standardized 1/4″ NPT vacuum breaker assembly, but poppet and spring specifications vary significantly. Contact your machine manufacturer directly—provide the serial number and model year. Aftermarket universal kits exist (e.g., stainless steel 1/4″ anti-siphon valves compatible with Ascaso, Astoria, Bezzera, Faema, La Marzocco, and Wega), but OEM components ensure exact tolerance matching.
Typical seal kit cost ranges from $12–35 USD; full assembly replacement (body + internals) costs $45–120 USD depending on manufacturer. Labor for professional service typically adds $80–150.
Preventative Maintenance & Long-Term Reliability Protocols
Mineral Deposit Prevention
Install an in-line water softener or reverse-osmosis (RO) system upstream of the espresso machine. Hard water (calcium + magnesium ions) accelerates poppet seat micro-pitting. Target water hardness should remain below 50 ppm CaCO₃ equivalents. Systems using municipal water in hard-water regions should budget for water treatment—ROI typically recovers within 12 months through reduced component replacement frequency.
Thermal Cycling Protocol
Allow 15–20 minutes of warm-up time before first use each day. Rapid pressure cycling (turning the pump on/off in quick succession) accelerates spring fatigue. Operate the machine in gentle, sustained cycles rather than aggressive on-off pulses—the vacuum breaker experiences lower stress and maintains poppet seat concentricity longer.
Inspection Intervals
Professional inspection every 18 months for machines in commercial use (150+ shots daily), or every 24–36 months for home use (10–30 shots daily). Document observations in a maintenance log: note pressure gauge readings, steam venting quality, and any audible changes. Early detection of spring pre-load loss allows planned maintenance rather than emergency downtime.
Frequently Asked Questions
Q1: My vacuum breaker hisses under load, but the pressure gauge reads stable. Is rebuild necessary?
Answer: Mild hissing (audible but not continuous) is normal as pressure nears setpoint—the poppet seat is transitioning from open to closed. Continuous high-velocity steam escape, or hissing that persists >2 seconds after pump stop, indicates poppet wear. Perform the pressure-drop test (Step 15): if the gauge holds ±0.1 bar over 2 minutes and steam venting is crisp and brief, the valve is functional and rebuild can be deferred. Monitor closely; degradation accelerates once micro-pitting initiates.
Q2: Can I replace only the spring without replacing seals?
Answer: No. Spring replacement almost always coincides with seal degradation because both components experience identical thermal stress. Reusing old seals with a new spring creates a weak failure point and voids the reliability benefits of spring replacement. Always purchase and install a complete rebuild kit (spring + all seals + poppet if available). Cost savings from partial replacement are minimal (<$3–5) and risk machine downtime.
Q3: My machine vents water droplets from the vacuum breaker outlet after shutdown. Is this a siphon-back emergency?
Answer: Water droplets indicate two possible conditions: (1) normal condensation if droplets appear only in the first 30 seconds post-shutdown, or (2) poppet seal failure if droplets continue intermittently over hours. Perform immediate pressure-drop validation (Step 15). If pressure drops >1 bar over 60 seconds, siphon-back risk exists—shut down the machine immediately and disassemble for inspection. Do not operate until the poppet is reseated or replaced. Siphon-back introduces water into the pump, causing cavitation noise and accelerated wear.









