Quick Answer: Solving How to Truing Flat Burr Carrier Flanges to <0.005mm (2026)
Flat burr carrier runout exceeding 0.005mm (0.0002″) occurs when the carrier flange deviates from perpendicularity to its rotational axis. Diagnose using a magnetic indicator stand with lever-style test indicator readable to ±0.01mm. Correct misalignment through precision shimming with calibrated stainless steel feeler gauge stock (0.05mm–0.15mm thickness), securing fasteners to specification torque, and validating results via multiple rotational measurements at three radial positions.
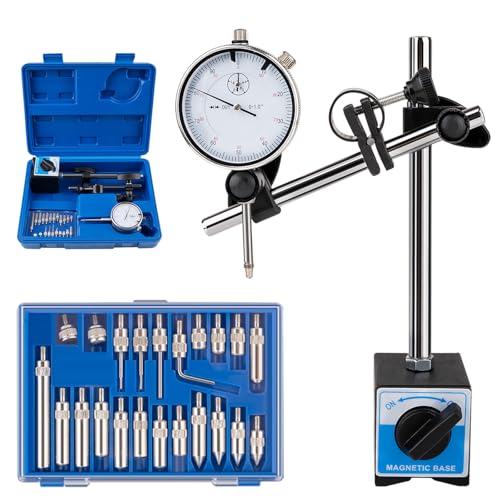
Pros
- Fine 0.001 inch graduation
- Adjustable long arm for flexible positioning
- Magnetic base for quick metal surface mounting
- Indicator and holder listed as one set
Cons
- Accuracy grade and build materials are not documented
- Magnetic hold may vary by surface type
This is a dial test indicator set with a magnetic base and adjustable long arm, listed for workshop, lab and mold making use. It is a practical option for a buyer who wants a basic setup for fine-increment readings, but the record does not confirm accuracy grade, materials or magnetic hold on specific surfaces, so those details should be checked before purchase.
- Measuring range: 0 to 1 inch
- Graduation: 0.001 inch
- Base: magnetic with adjustable long arm
- Listed use: workshop, lab and mold making

Pros
- Digital dial indicator format in the title
- Magnetic base included in the set
- Storage case included
- Gauge and base supplied as one set
Cons
- Measuring range and resolution must be confirmed before purchase
- Magnetic base may require a suitable ferrous mounting surface
This is a digital dial indicator kit with a magnetic base and storage case, suited to machinists, makers, and shop users who need a portable measuring setup. Confirm the measuring range, resolution, and accuracy in the full product documentation before relying on it for critical work.
- Product type: digital dial indicator gauge with magnetic base (per title)
- Package: storage case included (per title)
- Set contents: gauge and magnetic base (per title)
Root Cause Engineering & Mechanical Principles
Burr carrier runout—the radial and axial displacement of the flange as the carrier rotates—directly degrades grind uniformity in flat burr systems. When carrier flanges deviate from their theoretical perpendicular plane by more than 0.005mm, particle size distribution widens, extraction variance increases, and shot-to-shot consistency deteriorates. This mechanical eccentricity typically originates from manufacturing tolerances in the carrier body, fastener preload asymmetry, thermal expansion differentials, or wear in the drive shaft bushing. For detailed technical setup and system integration, reference our analysis on formulate sca water mineral buffers for espresso (2026).
Mechanical Failure Modes & Diagnostic Framework
| Symptom Presentation | Root Failure Mode | Diagnostic Tolerance (mm) | Typical Correction Method |
|---|---|---|---|
| Uneven grind particle size; fines accumulation on one side | Radial runout; carrier body eccentricity | >0.010mm TIR (total indicated runout) | Precision shim stack; carrier seat re-facing |
| Grinding noise or grinding burr drag at specific rotation angle | Axial runout; flange tilt or fastener preload mismatch | >0.008mm axial displacement | Calibrated feeler gauge shimming; fastener re-torque protocol |
| Grind setting creep; inconsistent shot pull timing | Combined radial + axial runout; thermal cycling | >0.015mm cumulative displacement | Multi-point shimming; thermal stabilization interval |
| Burr mounting surface corrosion; intermittent contact | Fastener corrosion; contaminated shim surfaces | >0.005mm micro-gap formation | Stainless steel shim replacement; fastener inspection |
Step-by-Step Diagnostic & Calibration Procedure
Phase 1: Equipment Setup & Baseline Measurement
Equipment Required:
- Magnetic indicator stand (ferrous mounting base)
- Lever-style test indicator with ±0.01mm resolution
- Precision feeler gauge set (0.05mm–0.25mm increment steps)
- Hex wrench set (5/16″ and 3/8″ minimum)
- Calibration arbor or pinned shaft retention tool
- Small steel alignment pins (2–3mm diameter, 40–60mm length)
- Torque wrench (0–15 N⋅m range)
- Soft brass or aluminum support block (burr protection)
Procedure:
- Isolate the carrier assembly. Remove the burr carrier from the grinder housing. Support the shaft with precision pins inserted into alignment holes or a retention bushing to prevent lateral deflection.
- Establish datum plane. Position the magnetic indicator stand 180° opposite the test point on the burr carrier’s outer flange edge. Mount the test indicator lever arm tangent to the flange surface at the carrier’s maximum radial distance (typically 20–35mm from centerline, depending on grinder model).
- Rotate through full cycle. Manually rotate the carrier shaft through 360°. Record the maximum indicator deflection (positive) and minimum deflection (negative). Total indicated runout (TIR) = Maximum deflection − Minimum deflection. Document in millimeters to two decimal places (e.g., 0.012mm TIR).
- Measure at three radial positions. Repeat steps 2–3 at 120° intervals around the flange circumference to identify asymmetric loading or localized bearing wear. Compare TIR values; variance greater than 0.003mm across positions indicates non-uniform shimming opportunity.
- Record baseline data. Photograph the dial indicator reading and document grinder model, carrier part number, and observed TIR. This baseline informs success metrics post-correction.
Phase 2: Root Cause Isolation & Shim Selection
Diagnostic Logic Tree:
- If TIR < 0.005mm: Runout within acceptable tolerance. Evaluate burr parallelism and espresso machine group head alignment as alternative grind uniformity culprits (refer to Specialty Coffee Association (SCA) specifications for extraction consistency benchmarks).
- If TIR = 0.005–0.012mm: Carrier-level runout is primary contributor. Proceed with single-sided or dual-sided shimming strategy (see Phase 3).
- If TIR > 0.012mm: Suspect bearing axial play, shaft deflection under load, or fastener preload asymmetry. Inspect bearing surfaces and fastener threads for damage before shimming.
Shim Selection Protocol:
Shims must be precision-ground stainless steel (304 or 316 grade) with parallelism tolerance ≤±0.01mm. Measure shim thickness using precision calipers or micrometer. Begin with a shim stack totaling 40–50% of measured TIR. Example: if TIR = 0.010mm, select shim combination yielding 0.004–0.005mm total thickness (e.g., one 0.003mm + one 0.002mm shim, or one 0.005mm shim). Position the stack under the fastener head or at the carrier seat bearing surface, based on grinder architecture.
Phase 3: Precision Shimming & Fastener Re-Torque
- Disassemble carrier fasteners. Remove hex screws or cap bolts securing the carrier body to the drive shaft. Note fastener depth, material (steel vs. stainless), and any existing shim stacks. Document original configuration photographically.
- Clean all contact surfaces. Wipe the carrier seat, shaft shoulder, and fastener heads with a clean, lint-free cloth. Remove any debris, corrosion, or old shim fragments. Do not use abrasive compounds; ISO 80 machine oil followed by a dry wipe suffices.
- Insert shim stack. Place the calibrated shim stack under the fastener head or between the carrier body and shaft shoulder. Ensure shims lie flat and are centered on the fastener axis to prevent tilting.
- Reinstall and hand-tighten fasteners. Thread fasteners by hand until they contact the shim stack. Do not force; stop when slight resistance is felt (indicating zero preload).
- Torque to specification. Refer to grinder manufacturer documentation for fastener torque spec (typical range: 4–8 N⋅m for M4–M5 fasteners). Apply torque in a star or cross pattern if multiple fasteners exist, to distribute preload uniformly. Re-check fastener tightness after each 1–2 N⋅m increment.
- Validate new TIR. Re-measure runout following the Phase 1 protocol. Target reduction to TIR < 0.005mm. If TIR remains > 0.008mm after shimming, suspect bearing wear or shaft damage; proceed to Phase 4.
Phase 4: Iterative Fine-Tuning & Acceptance Criteria
If initial shimming yields TIR = 0.006–0.008mm (marginal improvement), perform a secondary adjustment. Remove fasteners and add an additional 0.002–0.003mm shim. Repeat torque and measurement cycle. Acceptable final state: TIR ≤ 0.005mm at all three measurement positions, verified across a minimum of two 360° rotations under hand-applied load (no motorized rotation required).
Tools, Calibration Equipment & Component Replacement
Primary Diagnostic Instrumentation
- Magnetic Indicator Stand: Base footprint minimum 80mm × 120mm; magnetic clamping force ≥15 kg. Models with articulated arms and fine-adjust capability (e.g., Starrett 657AA series) reduce setup time and improve repeatability. Budget: $120–$280 USD.
- Lever Test Indicator: Resolution ±0.01mm (±0.0004″); range ±0.25mm minimum. Vertical or horizontal orientation lever style. Calibration certification recommended annually. Budget: $60–$150 USD.
- Precision Feeler Gauge Set: Stainless steel, 0.05mm–0.25mm thickness, steps of 0.01mm or 0.02mm. Individual blade thickness tolerance ±0.01mm. Avoid carbon steel sets (corrosion risk). Budget: $35–$75 USD.
- Metric Torque Wrench: 0–15 N⋅m range; ±4% accuracy class. Click-type wrenches suit grinder service work. Budget: $40–$90 USD.
Replacement Shim & Fastener Components
Order precision shims in mixed thickness packs (0.05mm, 0.10mm, 0.15mm, 0.25mm) from industrial fastener suppliers. Stainless steel 304 or 316 grade; thickness tolerance ±0.01mm. Fastener replacement: order original equipment manufacturer (OEM) hex cap screws or socket-head cap screws matching original size, thread pitch, and material. If fasteners exhibit corrosion or deformation, replace the complete set (typically 2–4 fasteners per carrier) rather than selective replacement, to ensure uniform preload distribution. For detailed technical setup and system integration, reference our analysis on rebuild commercial steam wand ball joints (2026).
Preventative Maintenance & Long-Term Reliability Protocols
Scheduled Inspection & Re-Verification
After completing burr carrier alignment, establish a preventative maintenance schedule. Perform TIR verification every 6 months or after grinding 200+ kilograms of beans—whichever occurs first. Monitor for grind consistency drift (expanding particle size range despite constant burr gap setting) as an early warning sign of degrading alignment. Document each measurement in a service log; trend analysis reveals gradual bearing wear or shim stack settling.
Thermal & Environmental Factors
Coffee grinder motors generate ambient heat; allow 30 minutes of idle time after extended grinding sessions before re-measuring runout. Thermal expansion of the carrier body and fasteners can temporarily increase TIR by 0.002–0.003mm. Conduct alignment verification in a stable 18–24°C environment. If a grinder is stored outdoors or in high-humidity conditions (RH > 75%), inspect stainless fasteners and shims quarterly for corrosion; salt spray or moisture can degrade surface finish and increase micro-gaps.
Fastener Preload Management
Fasteners securing the burr carrier tend to gradually loosen through vibration-induced self-loosening over hundreds of grinding hours. Every 12 months, re-verify fastener torque without disassembly: apply wrench to each hex fastener and confirm no rotational movement against the shaft. If fasteners have visibly loosened (rotating >15°), disassemble the carrier, inspect shim stacks for settling or debris intrusion, clean all surfaces, and re-torque to original specification. Replace fasteners exhibiting thread galling (raised material at thread edges) or stripping damage.
Frequently Asked Questions
1. Can I achieve <0.005mm runout without a magnetic indicator stand, using a lathe spindle or other precision equipment?
Magnetic indicator stands remain the industry standard for field-based burr carrier alignment because they require only a stable ferrous base surface—no specialized machinery. However, if access to a precision spindle (CNC or manual lathe with TIR ≤0.002mm) is available, the carrier can be mounted in a collet and verified using the lathe’s spindle runout gauge. This method suits commercial coffee service technicians or roastery operations with on-site machining resources. Ensure spindle taper and collet are clean and matched to carrier shaft O.D. tolerance. Advantage: <0.002mm TIR validation possible. Disadvantage: requires equipment investment and operator expertise.
2. What if the burrs touch or bind before reaching my normal grind setting after shimming?
Burr contact before normal grind setting indicates either (a) excessive shim thickness introduced, or (b) pre-existing burr parallelism error (upper and lower burrs misaligned by >0.05mm). Begin by reducing shim stack thickness by 0.002–0.003mm and re-torque. Re-test grind setting. If binding persists, remove all shims and evaluate burr mounting faces for flatness using a straightedge or optical flat. Micro-scratches, corrosion pitting, or thermal warping of the burr carrier seat typically manifest as contact problems unrelated to runout. Refer to grinder manufacturer’s burr alignment procedure for parallelism correction—typically involving upper burr carrier face re-facing or lower burr seat honing.
3. Should I shim on the top side (under the fastener head) or bottom side (between carrier body and shaft shoulder)?
Shim placement depends on grinder architecture. If fasteners are cap screws or hex bolts and the carrier body sits directly on a machined shoulder, shim placement under the fastener head distributes preload uniformly across the carrier face. If fasteners thread directly into the shaft, place shims between the carrier body OD and the shaft shoulder to maintain axial positioning. Most modern grinder designs favor bottom-side (carrier-seat) shimming, as this reduces fastener preload concentration and minimizes micro-bending of the carrier flange. Consult grinder service documentation for OEM-specified shim placement. When in doubt, shim the bottom side—this is the lower-risk configuration. For detailed technical setup and system integration, reference our analysis on clean clogged e61 gicleur flow restrictors (2026).
Conclusion
Achieving and maintaining flat burr carrier flange runout <0.005mm requires systematic measurement discipline, precision components (stainless steel shims and fasteners), and a repeatable verification protocol. The magnetic indicator stand and lever test indicator methodology outlined above delivers field-proven results at minimal cost and no specialty equipment beyond standard hex wrenches and a torque wrench. Routine re-verification every 6–12 months and attention to fastener preload management ensure long-term grind consistency and extend the operational life of both the carrier and the burr set. For espresso applications where extraction uniformity directly impacts shot quality, this level of precision alignment represents a justified investment in equipment reliability and beverage quality assurance.