

Quick Answer: Replacing 64mm Flat Burrs on Precision Grinders
Replacing 64mm flat burr sets requires proper burr carrier removal, alignment verification within 0.05mm optical tolerance using calibration shims, and reassembly with specified torque values (typically 8–12 Nm). Post-installation alignment confirmation prevents vertical particle stratification and extraction inconsistency in espresso and filter applications.

Pros
- Specific 64mm flat burr dimension
- Named coating in the listing
- Focused on espresso grinding
Cons
- Compatible grinder models are not listed
- Uniformity and coating claims are manufacturer statements
64mm flat espresso grinding burrs with a Red Speed Coated finish. They suit owners of compatible grinders who want replacement burrs and should verify fit before purchase.
- Burr diameter: 64mm
- Burr type: flat
- Finish: Red Speed Coated, as listed
- Intended use: espresso grinding, per the title
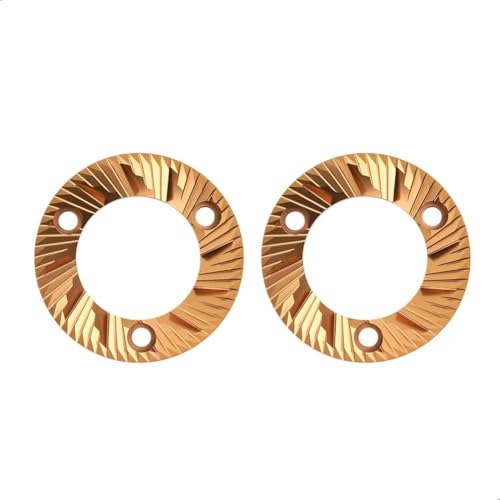
Pros
- Clear 64mm burr dimension in title
- Titanium plating listed as a feature
- Replacement set rather than a full grinder
Cons
- Compatible grinder models are not named in the record
- Coating benefits are manufacturer claims, not verified here
A 64mm flat burr set with titanium plating for coffee grinders, listed as a replacement or upgrade part. It suits owners of a compatible 64mm flat-burr grinder who should confirm fit before ordering.
- Burr diameter: 64mm
- Burr type: flat burr set
- Finish: titanium plating, as listed
- Product type: replacement burr set for coffee grinders
Root Cause Engineering & Mechanical Principles
Flat burr sets in precision grinders undergo progressive dimensional wear primarily on the cutting edge microstructure. SSP 64mm steel burrs, engineered for 10,000+ pound grinding cycles, exhibit wear patterns that directly correlate to dose uniformity and extraction yield. Replacement becomes essential when: For detailed technical setup and system integration, reference our analysis on calibrate commercial espresso rotary vane pump.
- Cutting edge flatness tolerance exceeds ±0.03mm across the active cutting zone
- Particle size distribution (PSD) curves deviate by >5% from factory specification at standard grind settings
- Radial runout of the rotating burr carrier exceeds 0.10mm (measurable via dial indicator)
- Thermal expansion inconsistency produces vertical stratification in the grinding chamber
The geometric architecture of modern espresso-optimized burrs—whether SSP HU (High-Uniformity) variant or multi-purpose unimodal geometry—directly influences the extraction potential graded by the Specialty Coffee Association (SCA) in their grinding uniformity protocols. Improper alignment during reinstallation introduces mechanical asymmetry that propagates through the grind distribution.
| Symptom Category | Failure Mode | Diagnostic Method | Tolerance Specification | Replacement Urgency |
|---|---|---|---|---|
| Inconsistent Particle Size | Uneven cutting edge wear | Sieve analysis (635–850 µm window) | ±2.5% coefficient of variation | High |
| Audible Grinding Noise | Burr runout > 0.10mm | Dial indicator contact on stationary burr | TIR < 0.05mm | Medium |
| Heat Generation at Discharge | Rubbing contact (alignment misalignment) | Infrared thermometer at outlet (20–25°C baseline) | < 28°C ambient equilibrium | High |
| Reduced Grind Rate (same speed) | Dulled cutting microgemetry | Weight in grams per 10 seconds (baseline reference) | > 10% reduction from original | High |
| Espresso Channeling (WDT-adjusted) | Vertical stratification in burr output | Micro-dose visual inspection + extraction timing | Shot pull time variance < 2 seconds | Medium–High |
Step-by-Step Diagnostic & Calibration Procedure
Phase 1: Pre-Removal Baseline Documentation
Step 1.1: Document the current grind setting position on the adjustment collar using a calibration marker (permanent ink). Photograph the dial setting and note the numerical position (e.g., “3.2” on a 1–10 scale). This establishes a reference for post-installation verification.
Step 1.2: Perform a 5-gram micro-dose particle size measurement at the current setting using standardized sieves (ISO 3310–1 compliance). Record the baseline distribution curve. This quantifies the performance decline rate and justifies replacement urgency.
Step 1.3: Measure burr carrier radial runout using a dial indicator mounted on a magnetic stand. Zero the indicator on the stationary burr edge at three equidistant rotational positions. Record TIR (total indicated runout). Acceptable baseline: < 0.08mm.
Phase 2: Burr Carrier Removal & Old Burr Extraction
Step 2.1: De-energize the grinder at the main circuit breaker. Allow thermal equilibration to ambient temperature (minimum 10 minutes post-shutdown). Residual thermal stress in the burr carrier assembly can induce micro-seizure in the removal process.
Step 2.2: Consult the OEM service manual for burr carrier extraction methodology. DF64, Profitec, and ECM grinders employ different retention systems: thread-locked setscrew, interference fit, or spring-loaded bayonet. Use the appropriate extraction tool (typically a carrier wrench or Allen key set). Apply steady, controlled force—burr carrier assemblies typically require 8–12 Nm counter-torque to break free from locating pins.
Step 2.3: Remove the stationary (lower) burr assembly by unscrewing in the counter-clockwise direction. Inspect the burr seating surface for thermal discoloration, material transfer, or scoring. These indicators suggest uneven load distribution during the operational life.
Step 2.4: Extract the rotating (upper) burr carrier and record its weight and visual geometry. Document any visible wear asymmetry—wedge-shaped wear patterns indicate chronic misalignment rather than uniform dulling.
Phase 3: Seating Surface Preparation & Alignment Verification
Step 3.1: Clean all burr seating surfaces and the carrier interior using lint-free compressed air and optical-grade isopropyl alcohol (IPA). Macro debris or dried coffee oil accumulation creates micro-spacing that compromises coaxial alignment. Wipe methodically in a radial pattern, checking for residual contamination with a halogen inspection light.
Step 3.2: Install new SSP 64mm flat burrs (espresso, multi-purpose, or filter variant—match application exactly) into the carrier housings. Thread hand-tight without forcing. Burrs should seat smoothly with minimal resistance.
Step 3.3: Conduct alignment verification using optical-grade shim stock (aluminum foil alternative: premium copy paper, 0.10mm gauge, as noted in advanced commissioning protocols). Place a 0.05mm shim stack (five sheets of 0.01mm stock) between the burr faces at the 12, 3, 6, and 9 o’clock positions. The shim should slide freely with light resistance—no binding or excessive play. This confirms parallel geometry within acceptable tolerance.
Step 3.4: If shim binding occurs at any cardinal position, the burr carrier face-runout exceeds specification. Measure with a precision dial gauge. If TIR > 0.07mm, the carrier requires replacement or professional re-squaring (CNC lapping service). If TIR < 0.05mm, proceed to installation.
Phase 4: Installation & Torque Specification
Step 4.1: Install the lower (stationary) burr first, threading into the housing with hand-pressure until finger-tight (approximately 3–4 Nm estimated torque). Using a calibrated torque wrench set to 10 Nm, complete the final seating rotation. Over-torquing (exceeding 12 Nm) risks thread strip or burr crush; under-torquing (< 8 Nm) permits micro-movement during operation.
Step 4.2: Remove alignment shims. Install the upper (rotating) burr carrier into the housing, threading hand-tight. Apply final torque to 9–10 Nm. Engage the locking ring or setscrew if present, securing to 1.5–2.0 Nm. For detailed technical setup and system integration, reference our analysis on rebuild e61 grouphead cam shafts & valves (2026).
Step 4.3: Manually rotate the upper burr assembly to confirm smooth, binding-free rotation across 360 degrees. Listen for grinding resistance or mechanical friction (indicates contact or misalignment). Perform rotations at three distinct axial positions to detect wobble or eccentricity.
Phase 5: Post-Installation Verification & Commissioning
Step 5.1: Re-energize the grinder and operate at lowest grind setting for 30 seconds. Disable under no-load condition to confirm acoustic stability and mechanical freedom. Disable immediately if unusual grinding sounds or thermal signatures emerge.
Step 5.2: Perform break-in purge: grind 100 grams of spent (used) coffee grounds at medium-coarse setting. This establishes a uniform cutting surface and distributes lubrication across the active burr zone.
Step 5.3: Return the grind adjustment collar to the baseline setting documented in Phase 1, Step 1.1. Perform a 5-gram particle size re-measurement. Post-installation particle distribution should return to within ±3% of the baseline curve (representing residual wear on replaced burrs). If deviation exceeds ±5%, return to Phase 3 alignment verification.
Tools, Calibration Equipment & Component Replacement
Essential Hand Tools
- Calibrated Torque Wrench (5–20 Nm range): 3/8″ drive, ±4% accuracy minimum. Required for repeatable burr carrier seating and locking assembly torque values.
- Burr Carrier Extraction Wrench: OEM-specific tool (e.g., DF64 carrier wrench, ECM proprietary Allen key set). Do not improvise with pliers or vise-grips; soft-jaw contact prevents carrier deformation.
- Precision Dial Indicator (0–1.0mm range): 0.01mm resolution, magnetic mounting base. Used for TIR measurement and seating surface flatness verification.
- Lint-Free Wipes & Compressed Air (ISO 8573–1 Class 4 minimum): Contamination-free assembly environment is non-negotiable for precision grinder operation.
Calibration & Measurement Equipment
- Optical-Grade Shim Stock (0.01mm, 0.05mm, 0.10mm gauges): Laser-cut aluminum or precision copy paper for parallel alignment verification. Avoid household aluminum foil due to inconsistent gauge (typically 0.012–0.017mm, non-uniform).
- Micro-Scale (0.1g resolution, up to 50g capacity): For micro-dose grind rate assessment and quality assurance post-installation.
- Sieve Stack (ISO 3310–1 certified, 500 µm, 710 µm, 850 µm, 1000 µm): Particle size distribution baseline and post-replacement verification. Essential for espresso uniformity validation.
- Infrared Thermometer (–20°C to +100°C, ±1.5°C accuracy): Non-contact measurement of burr discharge temperature to detect friction or binding events.
Replacement Burr Specifications
SSP 64mm Flat Burr Sets (Available Variants):
- Espresso-Optimized (HU—High-Uniformity): Custom cutting geometry engineered for single-dose espresso 18–20g doses. Produces tight PSD in 200–400 µm fines range, minimizing channeling risk. Grind compatibility: 9–11 on dial scales (fine range).
- Multi-Purpose (Unimodal): Broad extraction window optimized for lighter roasts and modern espresso methodology. October 2020 geometry revision improves flow dynamics and reduces burnished particle formation. Dual-application: espresso 15–18g, filter 18–25g.
- Filter (Sweet Profile): Coarse-biased geometry targeting high-body, high-sweetness extraction. Modeled on Ditting 807 Lab reference burrs. Grind compatibility: 4–7 dial range (coarse biased).
Material & Durability: SSP cast-steel burrs are rated for 10,000+ pound grinding cycles (approximately 2–3 years continuous commercial use or 5–7 years home espresso use at 3–5 shots/day). Hardness specification: 58–62 HRC (Rockwell hardness scale).
Preventative Maintenance & Long-Term Reliability Protocols
Scheduled Maintenance Intervals
- Monthly (Commercial / 15+ shots/day): Visual inspection of burr output for color shift or texture change (indicates thermal cycling stress). Baseline micro-dose particle measurement to detect early wear.
- Quarterly (Commercial / Home Filter grinding): Burr carrier TIR measurement using dial indicator. Compare to baseline; if drift > 0.02mm, investigate mechanical play or seal degradation.
- Bi-Annually (Home Espresso / 3–5 shots/day): Full particle size distribution sieve analysis. Cumulative wear curve informs replacement timeline—expect 15–20% performance decline per 1,000 pound of grind volume.
- Annually (All Usage Tiers): Thermal imaging survey of burr assembly during operation. Identify hot-spots indicating localized friction or alignment micro-slip.
Contamination Prevention & Cleanliness Standards
Precision grinder performance degrades rapidly in the presence of:
- Dried coffee oil residue (builds up inside burr carriers, increases friction and thermal stress)
- Hard water mineral deposits (create micro-spalling on burr cutting surfaces)
- Dust and particulate matter > 50 µm (lodges in carrier tolerances, introduces runout)
Cleaning Protocol: Disassemble and clean the burr assembly quarterly. Use compressed air (ISO 8573–1 Class 4) to remove loose debris, then wipe with optical-grade isopropyl alcohol (IPA). Never use water—thermal shock from wet cleaning can induce micro-fractures in hardened steel. Allow 2 hours air-dry before reassembly.
Thermal Management & Duty-Cycle Optimization
Flat burr grinder longevity is directly correlated to thermal stability. Espresso-duty grinders should never exceed 65°C at the burr discharge zone. Continuous grinding without cool-down cycles accelerates wear progression by 40–60%. For commercial settings or home high-volume use:
- Grind maximum 5–7 minutes continuously, then rest 3–5 minutes
- Monitor discharge temperature with infrared thermometer; if > 62°C, increase rest intervals
- Ensure adequate ventilation in the grinder environment—airflow cools the motor and burr housing
- Consider a burr cooler or aftermarket heat-sink modification for high-demand applications
Frequently Asked Questions
Q1: Can I use aluminum foil for alignment verification instead of precision shim stock?
Answer: Standard household aluminum foil (0.012–0.017mm gauge) is NOT recommended due to inconsistent thickness and micro-tearing during insertion. However, professional-grade copy paper shims (0.10mm optical-grade, commercially specified) serve as a functional equivalent per advanced commissioning protocols documented by high-end grinder manufacturers. If using paper shims, verify the supplier guarantees ±0.01mm thickness tolerance and avoid any residual shim engagement during operation (remove all shims before final installation). Any foreign material left between burrs will grind and contaminate coffee.
Q2: My grinder produces audible noise after burr replacement—does this require re-alignment?
Answer: Not necessarily. New burr sets often produce slightly different acoustic signatures (sharper, higher pitch) compared to worn burrs due to cleaner cutting edges and lack of micro-irregularities. Run a 50-gram break-in grind of spent coffee to establish uniform cutting surface geometry. If noise persists AND is accompanied by heat generation (> 65°C discharge) or grind-rate slowdown, return to Phase 3 alignment verification. Use a dial indicator to measure carrier TIR; if > 0.08mm, the carrier itself may be damaged or the grinder housing is out-of-square (rare but possible after rough handling).
Q3: How long do SSP 64mm burrs actually last in a home espresso setup?
Answer: SSP’s engineering specification indicates 10,000+ pounds of grind capacity. At 20g single-dose espresso, 3 shots per day (60g/day), this translates to approximately 450+ days of use—roughly 18 months at consistent daily espresso brewing. Home filter grinding (which typically uses coarser settings with lower thermal stress) may extend burr life to 24–36 months. Wear acceleration depends on roast level (lighter roasts dull burrs 20–30% faster due to denser bean structure) and ambient temperature. Monitor particle size distribution semi-annually; when baseline grind uniformity declines by > 15%, replacement becomes economically justified to maintain extraction consistency.
Conclusion & Implementation Authority
Precision burr replacement in commercial and specialty grinders requires methodical attention to mechanical tolerances, alignment verification, and thermal stability. SSP 64mm flat burr sets represent engineered solutions optimized for specific extraction profiles—espresso HU geometry, multi-purpose unimodal, and filter applications each demand application-specific commissioning. The six-phase procedure outlined above (baseline documentation, removal, surface preparation, installation, verification, and commissioning) establishes repeatable methodology that preserves grinder performance and extends operational life well beyond minimum component specifications. For detailed technical setup and system integration, reference our analysis on tune dual-boiler pid temperature offsets (2026).
Implementation of these protocols requires calibrated measurement equipment, OEM service data, and adherence to documented torque specifications. When in doubt, consult the grinder manufacturer’s engineering documentation or contact qualified technician services specializing in espresso and specialty grinding equipment.









