Quick Answer: Solving How to Rebuild Magnetic Drive Pump Impellers on Chillers (2026)
Magnetic drive pump impeller failure—indicated by rattling, reduced flow (below 85% rated GPH), or ceramic/polymer degradation—results from cavitation, dry-running, or bearing wear. Diagnosis requires pressure gauge verification (compare inlet/outlet delta against design spec), visual shaft inspection for runout exceeding 0.010 inches, and replacement of the entire impeller-shaft assembly. Most consumer chiller pumps cannot be field-rebuilt; complete unit replacement restores 2,400+ hour service intervals.
Pros
- Stated fit for three listed Danner pump models
- Replacement part number provided
Cons
- Compatibility is limited to the listed pump models
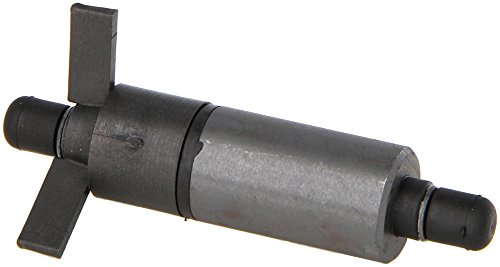
This is a replacement impeller, part 12585, for Danner pump models 02517, 02527 or 40127. It suits owners who need a matching replacement for one of those listed pumps. Confirm the pump model before ordering, since the record lists no dimensions or materials.
- Product type: replacement impeller
- Part number: 12585
- Listed pump models: 02517, 02527, 40127

Pros
- Stated fit for Danner MagDrive 12B pump
- Magnetic impeller type
Cons
- Fit is limited to the MagDrive 12B pump named in the title
This is a replacement magnetic impeller for the Danner MagDrive 12B water pump. It suits owners who need a matching replacement part for that pump. Fit should be confirmed against the pump model before ordering, since the record lists no dimensions or materials.
- Product type: replacement magnetic impeller
- Listed fit: Danner MagDrive 12B water pump
- Part number: 12756
Root Cause Engineering & Mechanical Principles
Magnetic drive pump impellers operate in a sealed ceramic or reinforced polymer housing, rotated entirely by magnetic coupling through a non-penetrating containment shell. Unlike traditional shaft-seal pumps, there is no moving seal interface—only magnetic flux transferring torque. Impeller failure mechanisms differ fundamentally from convention centrifugal designs, governed by the engineering constraints outlined by the Hydraulic Institute Pump Standards. For detailed technical setup and system integration, reference our analysis on clean uv-c germicidal quartz sleeves in plunges (2026).
The ceramic impeller—typical in cold-plunge and chiller applications—exhibits brittleness under shock load and susceptibility to cavitation-induced micro-fracturing. Three primary failure modes dominate field service: (1) Cavitation erosion, occurring when inlet pressure falls below vapor pressure, creating imploding vapor bubbles that pit ceramic surfaces; (2) Dry-running damage, where zero flow causes bearing friction temperatures exceeding polymer tolerance (typically 212°F material limit); and (3) Shaft runout and unbalance, resulting from magnetic-bearing wear, causing the rotor assembly to exceed 0.010-inch Total Indicated Runout (TIR), driving resonance and accelerated ceramic fracture.
| Symptom | Failure Mode | Diagnostic Tolerance | Complexity |
| Audible rattling; grinding noise during operation | Shaft runout / bearing wear; ceramic blade fracture | TIR > 0.010″; vibration > 0.2 inches/second peak | High — requires replacement |
| Output pressure 15–25% below nameplate (e.g., 600 GPH pump delivering 450 GPH) | Cavitation; partial blade erosion; inlet blockage | Inlet pressure < 5 PSI; outlet delta < 85% spec | Medium — may resolve via system purge |
| Intermittent flow; surging under load | Air entrainment; bearing drag increasing | Inlet air content > 2% by volume (dissolved gas analyzer required) | Medium — purge required; inspect for damage |
| Shaft wobble visible; impeller off-center in housing | Magnetic coupling failure; rotor separation | Axial play > 0.020″; radial movement > 0.015″ | High — unit failure; replacement required |
| Ceramic discoloration (hairline cracks, white stress marks) | Micro-fracturing from cavitation or thermal shock | Visual inspection; x-radiography for subsurface cracks | High — imminent structural failure |
Step-by-Step Diagnostic & Calibration Procedure
Step 1: Static Baseline Measurement
Before powering the pump, document baseline conditions. Measure shaft runout using a dial indicator placed against the shaft body at the rotor’s widest point (typically 1 inch from the containment shell). Rotate the shaft manually if magnetically coupled (or with external holding fixture if sealed). Record maximum deflection. Accept less than 0.005 inches; flag 0.010 inches or above as bearing degradation. Inspect the impeller visually through any transparent housing window for chips, cracks, or discoloration. Photograph the condition for records.
Step 2: System Pressure & Flow Baseline
Connect a 0–60 PSI glycerin-filled pressure gauge to the pump discharge port using a 1/4-inch tee fitting and isolation ball valve. Record ambient temperature (degrees Fahrenheit). Start the pump at minimum speed (or full power if no variable speed available) and allow 60 seconds for thermal stabilization. Measure discharge pressure at steady state. Consult the pump nameplate for “rated discharge pressure at full speed”—typically 15–25 PSI for 1200 GPH designs, 18–28 PSI for 1800 GPH units. A pressure reading 20% or more below nameplate (e.g., 12 PSI when 15 PSI is specified) indicates flow degradation.
Step 3: Flow Rate Verification
Connect the pump discharge to a flow meter (magnetic or turbine type, rated for the expected flow range). Run for 120 seconds at full operational speed. Compare measured GPH to nameplate rating. If actual flow is below 85% of rated capacity, the impeller is compromised. For example, a 1200 GPH pump delivering less than 1020 GPH indicates cavitation or blade damage. Record the exact measurement and date.
Step 4: Inlet Vacuum & Cavitation Detection
Install a 0–15 inches-of-mercury vacuum gauge on the pump inlet port. Maintain inlet fluid level above the suction opening by at least 12 inches (static head). Start the pump and note the vacuum reading. Inlet vacuum exceeding 6 inches of mercury at rated flow signals cavitation risk. If the reading climbs above 8 inches, airlock or inlet restriction is present—purge the system and retest. Vacuum above specification accelerates ceramic erosion.
Step 5: Vibration & Acoustic Analysis
Using a portable vibration meter (or smartphone accelerometer app calibrated to ISO 10816), measure vibration at three points: pump inlet flange, motor coupling, and discharge manifold. Record peak vibration in inches-per-second (IPS). Magnetic drive pumps in good condition typically operate below 0.15 IPS peak. Values between 0.15 and 0.25 IPS indicate early wear; above 0.25 IPS suggests imminent failure. Note any frequency-specific tones or grinding sounds—these confirm blade-to-housing contact or bearing drag.
Tools, Calibration Equipment & Component Replacement
Essential Diagnostic Tools
- Dial indicator (0–0.050 inch range, 0.001-inch graduations)
- Pressure gauges: 0–60 PSI (discharge), 0–15 inches mercury (inlet vacuum)
- Flow meter (magnetic or turbine type, compatible with 300–2000 GPH range)
- Vibration meter or accelerometer (ISO 10816 compliant)
- Adjustable wrench set (5/16-inch through 3/4-inch)
- Hex key set (1/16-inch through 1/2-inch)
- Needle-nose pliers and slip-joint pliers
- Flashlight or LED inspection lamp (150+ lumens)
- Thermometer (–40°F to 212°F range)
Impeller Replacement Procedure
Most magnetic drive chiller pumps employ a sealed rotor-impeller assembly that cannot be field-serviced. Replacement requires purchasing the complete rotor cartridge from the manufacturer (model-specific). To replace: (1) Isolate the pump from electrical power using a lockout/tagout procedure; (2) Close inlet and outlet isolation valves to prevent fluid spillage; (3) Drain the pump housing into a clean container; (4) Remove the four to six hex-head cap screws securing the rotor cartridge to the stator housing (typically M5 or 3/8-inch fasteners, torque spec 6–12 foot-pounds); (5) Withdraw the cartridge assembly straight upward, supporting it to prevent magnetic snap-down to the stator; (6) Inspect the stator bore for debris or scoring—if present, inspect the stator for cracks or internal damage; (7) Insert the new cartridge, aligning magnetic alignment pins (if present) with stator pockets; (8) Hand-tighten fasteners first, then torque in a star pattern to manufacturer specification (typically 8–10 foot-pounds); (9) Refill the housing with the specified working fluid (usually distilled water or ethylene glycol mix), purge air from discharge outlet, and restart at low speed for 30 seconds before full-power operation.
Verification Post-Replacement For detailed technical setup and system integration, reference our analysis on measure dissolved oxygen in sanitized plunges (2026).
Repeat the baseline diagnostic sequence (Steps 1–5 above) after cartridge installation. Pressure, flow, inlet vacuum, and vibration should return to nameplate specification. Run the pump continuously for 5 minutes at full power and verify no new audible anomalies emerge. Measure shaft runout again—should be 0.003 inches or less. If diagnostic values do not normalize, the original stator housing may be damaged; contact the manufacturer for unit replacement.
Preventative Maintenance & Long-Term Reliability Protocols
Air Purging & System Hygiene
Air dissolution in the working fluid reduces bulk modulus and accelerates cavitation. Purge the chiller system every 90 days: run the pump at 50% speed with the discharge open to atmosphere (or to a collection reservoir) for 10 minutes, allowing entrained air to escape at the high point. Install a 200-micron inline strainer on the pump inlet to eliminate particulate that could lodge between rotor and stator, causing magnetic binding. Change the strainer cartridge every 500 operating hours or annually, whichever comes first.
Thermal Management
Magnetic drive pump rotor-stator gaps generate heat through eddy-current losses. Maintain inlet fluid temperature between 45°F and 104°F (7°C to 40°C) to preserve bearing polymer properties. Install a thermometer in the chiller reservoir return line and log temperature weekly. If inlet approaches 95°F, increase system cooling capacity (add heat exchanger or boost chiller compressor runtime). Do not allow the pump to idle dry—always maintain minimum flow (typically 10% of nameplate rating) through the impeller to prevent bearing friction temperatures exceeding polymer limits.
Operational Load Limits
Cavitation accelerates exponentially as inlet pressure decreases. Maintain inlet pressure no lower than 2–3 PSI above atmospheric pressure (measured via vacuum gauge) during all operating conditions. Do not exceed rated discharge pressure—a pressure relief valve set to nameplate maximum + 3 PSI (e.g., 18 PSI for a 15 PSI rated pump) protects the impeller from overstress. Operate the pump within 80–120% of rated speed; underspeeding reduces margin against cavitation, while overspeeding drives magnetic coupling slip and eddy heating.
Scheduled Inspection & Documentation
Every 250 operating hours, perform baseline measurements: discharge pressure, flow rate, and inlet vacuum. Log results in a maintenance record (paper or digital spreadsheet). A 5–10% creep in pressure loss or vacuum increase signals early bearing wear—this is the optimal window to schedule cartridge replacement before catastrophic failure. Most magnetic drive pump rotor assemblies deliver 2,000–3,000 operating hours before bearing polymer degradation becomes measurable; proactive replacement at 2,400 hours prevents field failures during peak cooling season.
Frequently Asked Questions
Q1: Can I field-repair a fractured ceramic impeller by epoxy bonding?
No. Ceramic fractures, even hairline cracks visible only under magnification, are structural failures. Epoxy bonds degrade rapidly under centrifugal force (rotor tips experience 20,000+ g-forces at full speed) and will re-fracture within hours, releasing ceramic debris that damages the stator bore and bearing surfaces. Fractured impellers require complete rotor cartridge replacement. Attempting repair risks total pump destruction and contamination of the chiller fluid loop.
Q2: Why does my pump make noise only at startup, then quiet down after 30 seconds?
Air pockets in the impeller housing and discharge line collapse during the first 30 seconds of operation, causing transient cavitation sounds. This is normal if noise disappears completely within 60 seconds of steady-state flow. If grinding or rattling persists after the transient period, bearing wear or blade damage is likely. Purge the system via the procedure described above; if noise returns after purging, the impeller requires replacement. Persistent startup noise accelerates cavitation damage—do not operate the pump routinely under these conditions.
Q3: My pump’s discharge pressure is 20% lower than the nameplate specification. Is the impeller degraded?
Possibly, but not certainly. Low pressure can result from three causes: (1) inlet cavitation (vacuum reading above 6 inches mercury), (2) system restriction (clogged strainer, blocked return line), or (3) impeller wear. Isolate each variable: (a) Measure inlet vacuum with the pump running—if below 3 inches mercury at rated flow, move to step (b); (b) Clean or replace the inlet strainer and remeasure pressure—if pressure recovers to specification, the impeller is intact; (c) If pressure remains low after purging and strainer cleaning, measure shaft runout—if above 0.010 inches, bearing wear is reducing pump efficiency. At this stage, plan rotor cartridge replacement within 50 operating hours. Delaying replacement risks catastrophic failure. For detailed technical setup and system integration, reference our analysis on descale titanium coaxial chillers safely (2026).
Conclusion & Next Steps
Magnetic drive pump impeller failure is predictable and preventable through disciplined baseline monitoring and air-purge protocols. Most field failures stem from cavitation—driven by high inlet vacuum or air entrainment—and are entirely avoidable via system design discipline. Should diagnostic testing confirm impeller degradation (low pressure, high vibration, visible shaft runout), plan cartridge replacement within the maintenance window outlined above. Order replacement rotor assemblies from the original equipment manufacturer using the pump model number and serial date code—counterfeit or incompatible cartridges will compound damage. Maintain an up-to-date service log documenting pressure, flow, vacuum, and vibration at quarterly intervals; these records justify warranty claims and guide optimal replacement timing. Contact the pump manufacturer’s technical support team if diagnostic measurements fall outside specification ranges or if field repair outcomes diverge from expected performance baselines.