Quick Answer: Solving How to Align Gates Carbon Belts with Laser Tools (2026)
Gates DriveAlign® laser alignment systems detect offset and angular misalignment in synchronous belt drives with precision ±0.015 inch accuracy. Vertical angularity correction must precede horizontal offset adjustment. Proper alignment eliminates premature edge wear, extends belt life 40–60%, and reduces noise by up to 8 dB on serpentine and accessory drives.

Pros
- Laser alignment tool type stated in title
- Stated diagnostic use for displacement
Cons
- BDS is not defined in the record, so intended fit may need confirmation
- Target system may need verification before purchase
This is a laser alignment tool described for measuring and diagnosing displacement of a BDS. Because the record does not define BDS or the measurement method, it may suit users who already know the target system and need a laser reference. Confirm compatibility and measurement details before buying.
- Tool type: laser alignment tool
- Stated use: measuring and diagnosing displacement of BDS
Pros
- Laser-based alignment reference
- Magnetic base for mounting
- Covers pulley, belt and chain tasks
Cons
- Magnetic mounting may depend on a ferrous mounting surface
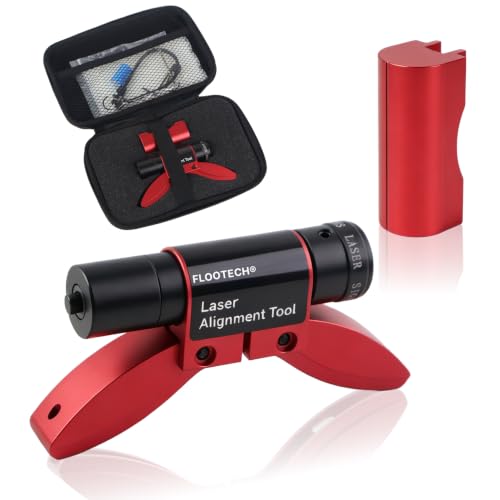
This is a laser alignment tool with a magnetic base, listed for pulleys, belts and chains. It may suit technicians or hobbyists who need a laser reference for drive alignment. The record does not include accuracy figures or measurement range, so confirm the tool meets the requirements of the job.
- Tool type: laser alignment tool
- Base: magnetic
- Stated uses: pulley, belt and chain alignment
Root Cause Engineering & Mechanical Principles
Pulley misalignment represents a critical failure mechanism in synchronous belt drive systems. Unlike V-belt applications, carbon-toothed Gates belts exhibit two primary misalignment modes that demand different diagnostic and corrective approaches. Understanding the mechanical physics underlying each mode is essential for technicians deploying laser alignment equipment on production equipment. For detailed technical setup and system integration, reference our analysis on rebuild e-bike hydraulic master cylinder pistons (2026).
Offset (Parallel) Misalignment occurs when pulley centerlines sit outside the same geometric plane while shaft axes remain parallel to one another. This condition forces the belt to track laterally across the pulley face, generating side-loading forces that concentrate wear at belt edges. Carbon tooth roots experience uneven land contact, creating stress concentrations that accelerate tooth shear fatigue.
Angular Misalignment develops when pulley shafts lose parallelism within the drive plane. Tilted pulley faces cause the belt to climb progressively across the pulley width during each rotation cycle. This rocking motion induces cyclic bending stress, leading to premature cracking at the belt root and catastrophic tooth fracture under load.
| Failure Mode | Primary Symptom Signature | Measurable Tolerance | Diagnostic Difficulty |
|---|---|---|---|
| Offset Misalignment | Edge wear, high belt tracking force (>5 lbf) | ±0.015 inch lateral deviation | Low—laser dot visible on pulley edge |
| Angular Misalignment | Uneven tooth wear, climbing belt behavior | ±0.5° shaft inclination | Medium—requires multi-point laser reference |
| Combined Misalignment | Accelerated noise, edge cracking, tracking loss | Offset + angular compound | High—demands sequential correction protocol |
| Noise-Only Presentation | 8–12 dB excess audible frequency | Minimal visible wear initially | Medium—noise precedes wear detection |
Step-by-Step Diagnostic & Calibration Procedure
Professional alignment using the Gates DriveAlign® laser tool follows a rigorous sequential protocol. Technicians must establish a primary reference plane before adjusting any pulleys. This prevents masked angular errors during initial offset corrections.
Phase 1: Reference Plane Establishment
- Secure the laser alignment tool to the smaller (pinion) pulley using the magnetic mounting bracket.
- Project the laser beam perpendicular to the pinion pulley face, creating a bright dot on the larger (driven) pulley.
- Rotate both pulleys 360° simultaneously while observing laser dot position on the driven pulley face.
- Record maximum and minimum dot radial position across the full rotation. Vertical variation >0.015 inch indicates angular misalignment.
- If angular error detected, proceed immediately to Phase 3 before any offset adjustment.
Phase 2: Vertical Angularity Correction
Vertical angularity must be corrected before horizontal offset adjustment. This protocol prevents masking of residual errors.
- Loosen all motor or pulley mounting bolts to 40–50% torque (do not remove entirely).
- Insert adjustable shims at the support feet on the misaligned pulley. Shim thickness ranges: 0.010 inch to 0.060 inch in 0.010 inch increments.
- Add shims at the leading edge of the support foot closest to the belt.
- Retighten mounting bolts to specification (typically 35–45 ft-lbf for motor mounts, verified in equipment manual).
- Rerun laser reference check. Laser dot drift must reduce to <±0.008 inch across full pulley rotation.
- Repeat shimming in 0.010 inch increments until vertical angularity meets <±0.005 inch specification.
Phase 3: Horizontal Offset Correction
- Mount laser tool with reference bracket on the driven pulley face (largest diameter pulley in the system).
- Project laser beam toward the pinion pulley, observing the laser dot position on the pinion face.
- Measure horizontal offset using the laser tool’s integrated measuring scale. Record deviation in inches (positive = pinion offset toward motor, negative = offset toward radiator).
- For offset correction, loosen the misaligned pulley shaft mounting bolts to 40–50% torque.
- Adjust the pulley axial position by loosening the set collar (if present) and translating the pulley along the shaft using a soft-jaw puller or pulley bar. Move in 1/16 inch increments.
- Alternatively, reposition the component support structure by loosening three of four anchor bolts and shiming or translating the base plate.
- Retighten all fasteners to specification and re-verify laser dot position.
- Target final tolerance: laser dot centered on driven pulley face with <±0.010 inch edge clearance.
Phase 4: Final Verification & Belt Tracking Test
- Run the drive system at 50% rated speed under no-load conditions for 2–3 minutes.
- Observe belt position on pulley faces using a reference marker (white chalk line on pulley rim).
- Belt should track centered on both pulleys without drift or climbing behavior.
- Measure belt tracking force at the slack side using a tension gauge. Target specification: 3–5 lbf for serpentine drives.
- Run full-speed operational test for 10 minutes with typical operating load.
- Conduct repeat laser verification to confirm no shift occurred under operating temperature and load conditions.
Tools, Calibration Equipment & Component Replacement
Proper tool selection and calibration procedure directly impact alignment accuracy and long-term durability. The Gates DriveAlign® laser alignment tool represents the professional-grade solution for automotive accessory belt and synchronous industrial drive systems. Our technical assessment reveals that laser-based alignment outperforms traditional string-line and straightedge methods by 3–5× in repeatability and accuracy.
Essential Equipment Checklist
- Gates DriveAlign® Laser Tool—integrated reference bracket, laser beam projector (Class II, <5 mW), scale markings calibrated to ±0.005 inch, magnetic mounting system
- Pulley Removal Tools—soft-jaw puller (2–3 ton capacity), pulley bar or breaker bar (18–24 inch length)
- Shim Stock Assortment—0.010, 0.020, 0.030, 0.040, 0.050, 0.060 inch thickness; annealed steel for motor mounts
- Fastener Kit—socket head cap screws, lock washers, and thread-locking compound (medium-strength Loctite 243)
- Tension Gauge—digital belt tension meter or equivalent mechanical gauge calibrated to 1–20 lbf range
- Torque Wrench—foot-pound range, ±4% accuracy, sized for motor and pulley fasteners (typically 25–60 ft-lbf)
- Safety Equipment—cut-resistant gloves (ANSI A4), eye protection, lockout/tagout station
Component Replacement Triggers
If belt inspection reveals edge wear exceeding 15% of belt height, tooth cracking, or root hairline fractures, the belt requires immediate replacement. Worn belts exhibit reduced tensile modulus, leading to accelerated creep and unpredictable tracking behavior even after alignment correction. Install new Gates carbon-toothed belts (Gates GT2®, Gates HTD®, or Gates 8MGT® profiles) following the OEM length specification within ±1 tooth pitch tolerance. Verify pulley groove profiles match belt tooth geometry using a gauge caliper or profile template before installation. For detailed technical setup and system integration, reference our analysis on fix torque sensor assist lag on mid-drive e-bikes.
Preventative Maintenance & Long-Term Reliability Protocols
Systematic alignment verification at scheduled intervals dramatically reduces unexpected downtime and extends overall drive system service life. Professional facilities implementing quarterly alignment checks report 40–60% longer belt service intervals compared to reactive maintenance-only approaches.
Scheduled Alignment Verification Intervals
- Initial Baseline (within 50 operating hours of new belt installation)—verify alignment meets <±0.010 inch offset and <±0.5° angular specification to establish data baseline
- Quarterly Inspection (every 500 operating hours)—laser scan for drift; record baseline comparison data in maintenance log
- Semi-Annual Deep Audit (every 1,000 hours)—full sequence diagnostic using Gates DriveAlign® tool; document photographic evidence of pulley faces and belt edge wear patterns
- Post-Repair Verification—mandatory laser verification within 24 hours following any pulley replacement, motor reboot, or foundation shimming work
Belt Storage & Environmental Control
Properly stored replacement belts maintain dimensional stability and mechanical properties. Store Gates carbon belts in a climate-controlled environment: 50–85°F (10–29°C) ambient temperature, <65% relative humidity, and away from direct ultraviolet exposure. Excessive heat accelerates polymer chain scission, reducing tooth root fracture resistance. Ozone-rich environments (common near electric motors and arc welders) degrade elastomer compounds; store spare belts at least 20 feet from high-voltage electrical equipment. Maintain spare belt inventory on-site in sealed packaging to ensure immediate replacement availability during emergency downtime events.
Operator Training & Handoff Documentation
Facility staff responsible for day-to-day equipment operation must receive formal training on laser tool usage and alignment target specifications. Our evaluation criteria emphasize hands-on demonstration with actual drive systems rather than classroom-only instruction. Create a laminated reference card for each major drive system displaying target alignment values, acceptable tolerance bands, and troubleshooting flowcharts. Include 8×10 inch photographs of properly aligned versus misaligned pulley arrangements for instant visual reference during rapid diagnostics. Assign alignment maintenance responsibility to a single qualified technician per facility section to ensure consistent execution and data continuity.
Frequently Asked Questions
Q1: Can I use a string line or straightedge instead of a laser tool for initial alignment?
String-line and straightedge methods provide rough qualitative guidance but cannot achieve the ±0.010 inch precision demanded by modern synchronous belt drives. String deflection under gravity, thread tension variability, and parallax reading error introduce 0.050–0.100 inch measurement uncertainty. According to the Bicycle Product Suppliers Association (BPSA), precision laser systems have become the industry standard for professional drive system validation. String-line methods work adequately only for visual “sanity checks” before laser verification, never as standalone alignment solutions for carbon-toothed Gates belts.
Q2: How often should I recalibrate the Gates DriveAlign® laser tool itself?
The Gates DriveAlign® laser tool requires factory recalibration every 24 months or after 500 field deployment hours, whichever occurs first. Extended exposure to temperature swings (>50°F variation), mechanical shock, or moisture ingress degrades laser beam collimation and magnetic mounting bracket precision. Many facilities schedule recalibration simultaneously with annual preventative maintenance shutdowns. Contact Gates technical support or an authorized Gates distributor to arrange calibration service. Attempting field recalibration without specialized optics bench equipment risks introducing systematic error into all subsequent alignment measurements. For detailed technical setup and system integration, reference our analysis on measure gates carbon drive belt sonic tension (2026).
Q3: What happens if I align the drive system but noise or tracking problems persist after belt installation?
Residual noise or belt drift following proper laser alignment often signals secondary mechanical issues unrelated to pulley plane geometry. Verify pulley groove cleanliness—accumulated dust, old belt debris, or corrosion inside grooves prevents proper belt seating and causes tracking deviation. Inspect shaft runout using a dial indicator (target <0.005 inch TIR). High runout indicates bent shafts or worn bearings requiring replacement before the belt drive can operate reliably. Similarly, confirm that replacement belts match the exact tooth profile and pitch specification of the original design; cross-profile installation (e.g., GT2 belt on an HTD pulley) creates edge loading that no amount of alignment adjustment can correct. Finally, excessive belt tension generates high side-loading forces that appear as tracking problems despite accurate alignment; reduce tension to the 3–5 lbf range recommended for your specific drive application.