Quick Answer: Solving How to Balance Centrifugal Blower Wheels on Purifiers (2026)
Centrifugal blower vibration stems from mass imbalance—unequal weight distribution causing eccentric rotation. Diagnosis requires measuring vibration velocity at bearing housings using ISO 20816 standards (typically 0.28–0.71 in/sec acceptable range). Correction involves calculating required counterweight mass and angular position, then applying balance corrections via inlet ring modification or weight addition. Preventative maintenance includes quarterly filter inspection, bearing lubrication protocols, and biennial dynamic balancing verification.

Pros
- Low-profile, easy-peel adhesive design listed
- Black finish listed
- Six-strip box for multiple jobs
- Listed for cars, SUVs and motorcycles
Cons
- Adhesive durability and weight accuracy are not supplied
- Listed uses include crafts, so vehicle suitability needs checking
These are black, low-profile, adhesive stick-on weights listed in a 5gr size and packed six strips to a box. They suit buyers who want adhesive balancing weights for listed vehicles and can confirm the size and surface before use. The record does not confirm adhesive durability or weight accuracy, so review those details in the full listing.
- Weight size: 5gr, as listed
- Color: black
- Type: adhesive stick-on wheel weights, easy peel
- Packaging: 6 strips per box, as listed
- Origin: Korean Made, as listed
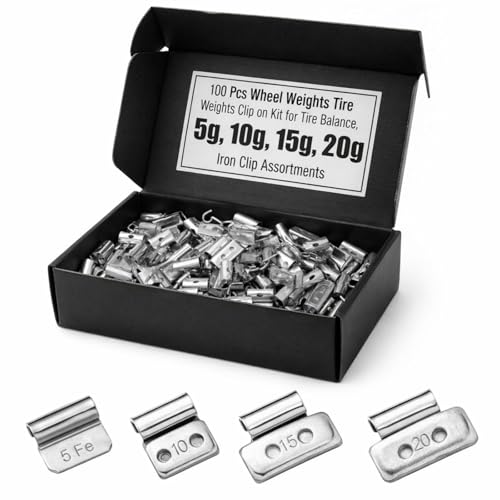
Pros
- 100 pieces across four listed weight sizes
- Clip-on style for tire balancing use
- Includes a box for storing assorted weights
Cons
- Rim type compatibility is not supplied in the record
- Clip style may not suit all rim types
- Weight accuracy and finish are not independently verified
This is a 100-piece assortment of clip-on iron tire weights in four listed sizes, from 0.18 oz to 0.7 oz. It suits buyers who balance tires or wheels and want a range of weights on hand. Because the record does not confirm rim compatibility or weight accuracy, check the clip style against your wheels before use.
- Quantity: 100 pieces total
- Listed weights: 0.18 oz, 0.35 oz, 0.5 oz, 0.7 oz
- Pieces per style: 25 (as listed)
- Material: iron clip, as listed
- Packaging: with box, as listed
Root Cause Engineering & Mechanical Principles
Centrifugal blower wheel vibration originates from a fundamental mechanical imbalance—uneven mass distribution around the wheel’s rotational axis. During rotation, each particle of the blade assembly and hub generates centrifugal force. When mass distribution is uneven, these forces do not cancel symmetrically, creating a resultant force that acts eccentrically. This eccentric loading forces the bearing housings and mounting structure to respond cyclically at blade-pass frequency (wheel RPM × blade count) and rotational frequency, generating audible noise and mechanical stress. For detailed technical setup and system integration, reference our analysis on descale ultrasonic piezoelectric transducers (2026).
Vibration manifests in two primary planes—axial (along the shaft) and radial (perpendicular to the shaft). Radial imbalance produces the dominant vibration signature in most purifier applications. The severity depends on three factors: mass offset magnitude, rotation speed, and bearing compliance. According to the Air Movement and Control Association (AMCA), tolerance for rotating machinery in HVAC applications falls within ISO 20816 classifications, with acceptable vibration velocity thresholds ranging from 0.28 to 0.71 inches per second depending on machine class and bearing type.
| Symptom/Failure Mode | Root Cause | Diagnostic Gauge/Tolerance | Resolution Difficulty |
|---|---|---|---|
| Audible humming or rattling at startup | Gross imbalance (>5 gram-inches) | Vibration velocity >1.0 in/sec; check with accelerometer at 0.5–2 kHz | Moderate—requires two-plane dynamic balancing |
| Resonant peaks within 5 minutes of operation | Resonance excitation near critical speed | Frequency sweep 0–1,200 RPM; identify peak amplitude | High—may require structural stiffening or bearing replacement |
| Bearing temperature rise (>15°F above baseline) | Excessive radial load from unbalance | Infrared thermometer; acceptable <150°F at bearing surface | High—indicates imminent bearing wear |
| Filter clogging acceleration | Contamination from bearing wear; imbalance debris | Pressure differential gauge; delta-P <1.5 inches H₂O when clean | Moderate—clean wheel and inspect for cracks |
| Intermittent vibration spikes | Partial blade damage or foreign object lodged | Visual inspection at 500× magnification; run-down test for 30 seconds | Moderate to High—wheel replacement may be required |
| Low-frequency rumble (subsonic) | Bearing radial play or hub looseness | Dial indicator runout <0.010 inches at hub; axial play <0.005 inches | Moderate—requires bearing or hub retightening |
Step-by-Step Diagnostic & Calibration Procedure
Phase 1: Pre-Balancing Inspection Protocol
Step 1: Visual and Mechanical Verification — Power down the unit completely and lock out all electrical circuits. Manually rotate the shaft using a tool or motor coupling, feeling for resistance, grinding, or binding. Inspect all blade leading and trailing edges for cracks, dents, or corrosion at 500× magnification or bright-light inspection. Remove any visible dust, lint, or debris from blade surfaces using compressed air (max 50 PSI) or soft brush. Check wheel-to-housing clearance at three circumferential positions—acceptable clearance is 0.10–0.20 inches.
Step 2: Filter Condition Assessment — Measure static pressure drop across the filter using a digital differential pressure gauge. Clean filters should read <1.0 inches H₂O; contaminated or clogged filters artificially inflate vibration measurements by restricting airflow and increasing rotational load. Replace filter if delta-P exceeds 1.5 inches H₂O, then allow motor to cool for 15 minutes before proceeding to vibration measurement.
Step 3: Bearing and Hub Runout Verification — Using a magnetic dial indicator mounted on a rigid stand adjacent to the motor shaft, measure total indicator runout (TIR) at the hub body approximately 1.0 inch from the wheel face. Acceptable TIR is <0.010 inches. If TIR exceeds 0.015 inches, the hub is bent or shaft is bowed—wheel replacement is necessary. Check axial play (end-to-end movement along shaft axis) using a dial indicator mounted axially; play should not exceed 0.005 inches. Excessive axial play indicates bearing wear.
Phase 2: Dynamic Vibration Measurement
Step 4: Baseline Vibration Assessment — Attach a portable vibration meter (accelerometer or velocity transducer) to the bearing housing using a magnetic mounting pad, positioning the sensor perpendicular to the radial direction of suspected imbalance. Power on the purifier and allow it to reach steady-state operation (typically 2–3 minutes). Record vibration velocity in inches per second (in/sec) at three bearing locations: motor-end bearing, blower-end bearing, and center bearing bracket. Document readings at both 1× rotational frequency (RPM ÷ 60) and 2× frequency.
Step 5: Frequency Spectrum Analysis — Using a handheld FFT analyzer or smartphone-based vibration app, perform a frequency sweep from 0 to 2,000 Hz. Identify dominant peaks at blade-pass frequency (BPF = wheel RPM × number of blades). For a typical eight-blade purifier wheel operating at 1,000 RPM, BPF = 133 Hz. If peak amplitude at BPF exceeds 0.5 in/sec in the radial direction, dynamic balancing is required. Record the precise frequency and amplitude of the dominant peak for reference during balancing calculations.
Phase 3: Imbalance Calculation and Correction
Step 6: Balance Weight Calculation — The corrective mass required is calculated using the formula: Required Mass (grams) = (Measured Eccentricity × Motor Mass) ÷ Correction Radius. Typical values: if measured vibration velocity is 1.2 in/sec on a motor with 15 kg total rotating mass, and the correction radius is 6.0 inches from the rotation center, the required balance mass is approximately 8–12 grams at a specific angular position. This calculation assumes a single-plane dynamic balance; two-plane balancing (axial and radial corrections) may be required for severe imbalances.
Step 7: Trial Weight Application and Verification — Using a precision scale (±0.1 gram resolution), measure the calculated balance weight (typically 5–15 grams for residential purifiers). Temporarily attach the weight to the wheel using high-temperature silicone adhesive or clamping fixture at the calculated angular position—use a protractor or angle finder to establish exact position. Restart the unit and immediately record vibration velocity using the same measurement methodology from Step 4. If vibration reduces by >50%, the balance weight placement is correct. If vibration increases or remains unchanged, the angular position is incorrect; rotate the weight 90° and re-test.
Step 8: Permanent Correction Method Selection — For residential purifiers, the preferred method is modification of the inlet ring—this involves adding a small lip or deflector element on the opposite side of the detected imbalance. Alternatively, permanent balance weights can be epoxied (two-part structural epoxy, 5-minute set) to the wheel at the verified position and allowed to cure for 24 hours before operation. Never use adhesive-backed tape or temporary fasteners; vibration will dislodge them.
Tools, Calibration Equipment & Component Replacement
Essential Diagnostic Instruments: For detailed technical setup and system integration, reference our analysis on detect chemical breakthrough in carbon filters (2026).
- Portable Vibration Meter — Digital accelerometer or velocity transducer (ISO 20816 compliant); required accuracy ±5%. Examples include Extech VB500, Fluke 805, or equivalent smartphone-based apps calibrated to factory standards. Cost range: $150–$800.
- Dial Indicator — Precision magnetic-base dial indicator with 0.001-inch resolution for runout and clearance measurement. Resolution accuracy must be <0.0005 inches. Cost: $40–$120.
- Digital Differential Pressure Gauge — Measures filter delta-P with ±0.1 inches H₂O accuracy. Cost: $80–$250.
- FFT Analyzer or Frequency Spectrum Analyzer — Handheld or smartphone-based tool for identifying dominant vibration frequencies. Must resolve to 1 Hz minimum. Cost: $200–$1,500.
- Precision Weight Scale — Digital laboratory balance with ±0.1 gram resolution. Cost: $50–$200.
- Infrared Thermometer — Non-contact temperature measurement for bearing thermal assessment. Resolution ±2°F. Cost: $30–$150.
Corrective Materials & Component Replacement:
- Precision Balance Weights — Pre-manufactured tungsten or steel weights (5–20 grams) for temporary trial balancing. Cost: $2–$8 per weight.
- High-Temperature Epoxy Adhesive — Two-part epoxy rated to 250°F for permanent weight attachment. Cure time: 24 hours. Cost: $12–$30 per kit.
- Replacement Bearing Assembly — If radial play exceeds 0.010 inches or bearing temperature rises >20°F, bearing replacement is required. Typical ball bearing cost: $40–$150 per bearing.
- Replacement Centrifugal Wheel — Complete wheel assembly (blade disk + hub) if wheel runout exceeds 0.020 inches or blade cracks are detected. Cost: $180–$450 depending on purifier model.
- Filter Media — Replacement filters should be installed simultaneously during balancing work. Cost: $25–$75 per filter.
Preventative Maintenance & Long-Term Reliability Protocols
Quarterly Maintenance Intervals: Inspect the centrifugal wheel visually every three months for dust accumulation, corrosion, or blade damage. Measure filter differential pressure and replace if delta-P exceeds 1.5 inches H₂O. Manually rotate the shaft without power to verify smooth operation; any grinding sensation indicates bearing wear. Clean wheel surfaces with a soft brush and compressed air at <50 PSI to remove dust and lint that could alter mass distribution over time.
Semi-Annual Lubrication and Electrical Verification: At six-month intervals, apply bearing lubrication per manufacturer specifications (typically NLGI Grade 2 multipurpose grease, 2–3 drops at lubrication port). Measure bearing temperature after 30 minutes of operation—acceptable temperature is <150°F. Perform a quick vibration check using a portable meter to detect any trending increase in vibration velocity, which may indicate early bearing wear or imbalance development.
Biennial Dynamic Balancing Verification: Every two years, perform the complete vibration measurement protocol outlined in Phase 2 above. If vibration velocity has increased by >20% compared to the previous measurement, initiate rebalancing procedures before vibration exceeds 0.71 in/sec. This proactive approach prevents accelerated bearing wear and extends motor life by 30–50% compared to reactive repair strategies.
Environmental Controls: Centrifugal wheel imbalance is accelerated by environmental factors—excessive humidity, temperature cycling, and corrosive airborne particles (salt air, industrial pollutants) can induce micro-corrosion and structural degradation. Maintain indoor storage humidity between 30–60% RH. For purifiers deployed in corrosive environments (coastal regions, industrial zones), consider stainless-steel wheel upgrades or protective coatings as proactive measures.
Frequently Asked Questions
Q1: Can I balance a centrifugal blower wheel using trial and error, or is precision equipment mandatory?
A: Trial and error is inefficient and unreliable for achieving vibration tolerances below 0.5 in/sec. Precision vibration measurement equipment (accelerometer or velocity transducer) is essential for three reasons: (1) human hearing cannot accurately quantify vibration magnitude—what feels like a small improvement may represent only 10–15% vibration reduction, (2) angular position errors as small as 10–15° can reverse the balancing effect, and (3) multi-plane imbalances require simultaneous measurement at multiple bearing locations to prevent over-correction in one plane while neglecting another. Professional balancing shops invest $2,000–$5,000 in diagnostic equipment because the return on investment through improved customer satisfaction and repeat service is substantial. For residential applications, rental of portable FFT analyzers ($40–$60 per day) is cost-effective.
Q2: How do I distinguish between imbalance vibration and vibration caused by loose mounting bolts or bearing wear?
A: Frequency analysis is the diagnostic key. Pure imbalance produces vibration at 1× rotational frequency (e.g., 16.7 Hz for a 1,000 RPM wheel). Loose mounting bolts generate sub-harmonic frequencies (0.5× to 0.8× running frequency) and broadband noise across multiple harmonics. Bearing wear produces high-frequency noise (>3,000 Hz) with rapid spectral fluctuation and intermittent spikes. Using an FFT analyzer, capture a frequency spectrum 0–2,000 Hz and identify the dominant peak location. If the peak is precisely at 1× frequency, imbalance is the primary issue. If multiple peaks exist across 0.5×–3.0× frequency range, tighten all mounting bolts and bearing fasteners (typical torques: M8 = 18–22 N·m, M10 = 30–36 N·m) and re-measure. Bearing wear is confirmed if high-frequency noise persists after bolt tightening.
Q3: After balancing, vibration improved significantly but hasn’t reached the target ISO 20816 tolerance of 0.28–0.45 in/sec. Should I attempt further balance corrections, or investigate other issues? For detailed technical setup and system integration, reference our analysis on gasket filter access doors to prevent leakage (2026).
A: If vibration has improved by >50% but remains above target tolerance, investigate these secondary factors before attempting additional balancing: (1) verify bearing axial play using dial indicator—play >0.008 inches indicates bearing degradation requiring replacement rather than further balancing, (2) check filter differential pressure—clogged filters artificially elevate vibration readings and can account for 0.15–0.25 in/sec of measured vibration, (3) inspect inlet ductwork for resonances or loose sections that may be amplifying wheel vibration, and (4) measure motor soft-foot (uneven contact between motor feet and mounting surface)—soft-foot >0.003 inches introduces structural resonances. Address the highest-impact issue first (typically bearing replacement or filter cleaning), then remeasure. If vibration remains >0.5 in/sec after these corrections, the wheel may have structural damage (micro-cracks or blade curvature degradation) requiring replacement. Attempting further balancing weight additions without addressing root causes is economically inefficient and may degrade balance rather than improve it.